

What Is an Elevator Counterweight Block and How It Works
In a traction elevator system, balance and efficiency are achieved through the use of a counterweight system. One of the most important components within this system is the elevator counterweight block. Although it is rarely seen by passengers, this component plays a critical role in ensuring smooth, stable, and energy-efficient elevator operation.
The elevator counterweight block is a solid mass, typically made of cast iron or concrete, installed inside the counterweight frame. Its primary function is to balance the weight of the elevator car along with a portion of the rated load. By doing so, it significantly reduces the amount of work that the elevator motor must perform.
In a typical configuration, the counterweight is designed to equal the weight of the elevator car plus approximately 40% to 50% of the maximum load. This balance allows the elevator system to operate more efficiently, especially during normal usage when the car is partially loaded.
When the elevator moves, the counterweight travels in the opposite direction of the elevator car. As the car goes up, the counterweight moves down, and vice versa. This balanced movement reduces energy consumption and minimizes wear on mechanical components such as the traction sheave and motor.
The structure of the counterweight block must be designed to withstand continuous movement and vibration. High-density materials are used to ensure that sufficient weight can be achieved within a limited space. Cast iron is one of the most commonly used materials due to its durability, density, and cost-effectiveness.
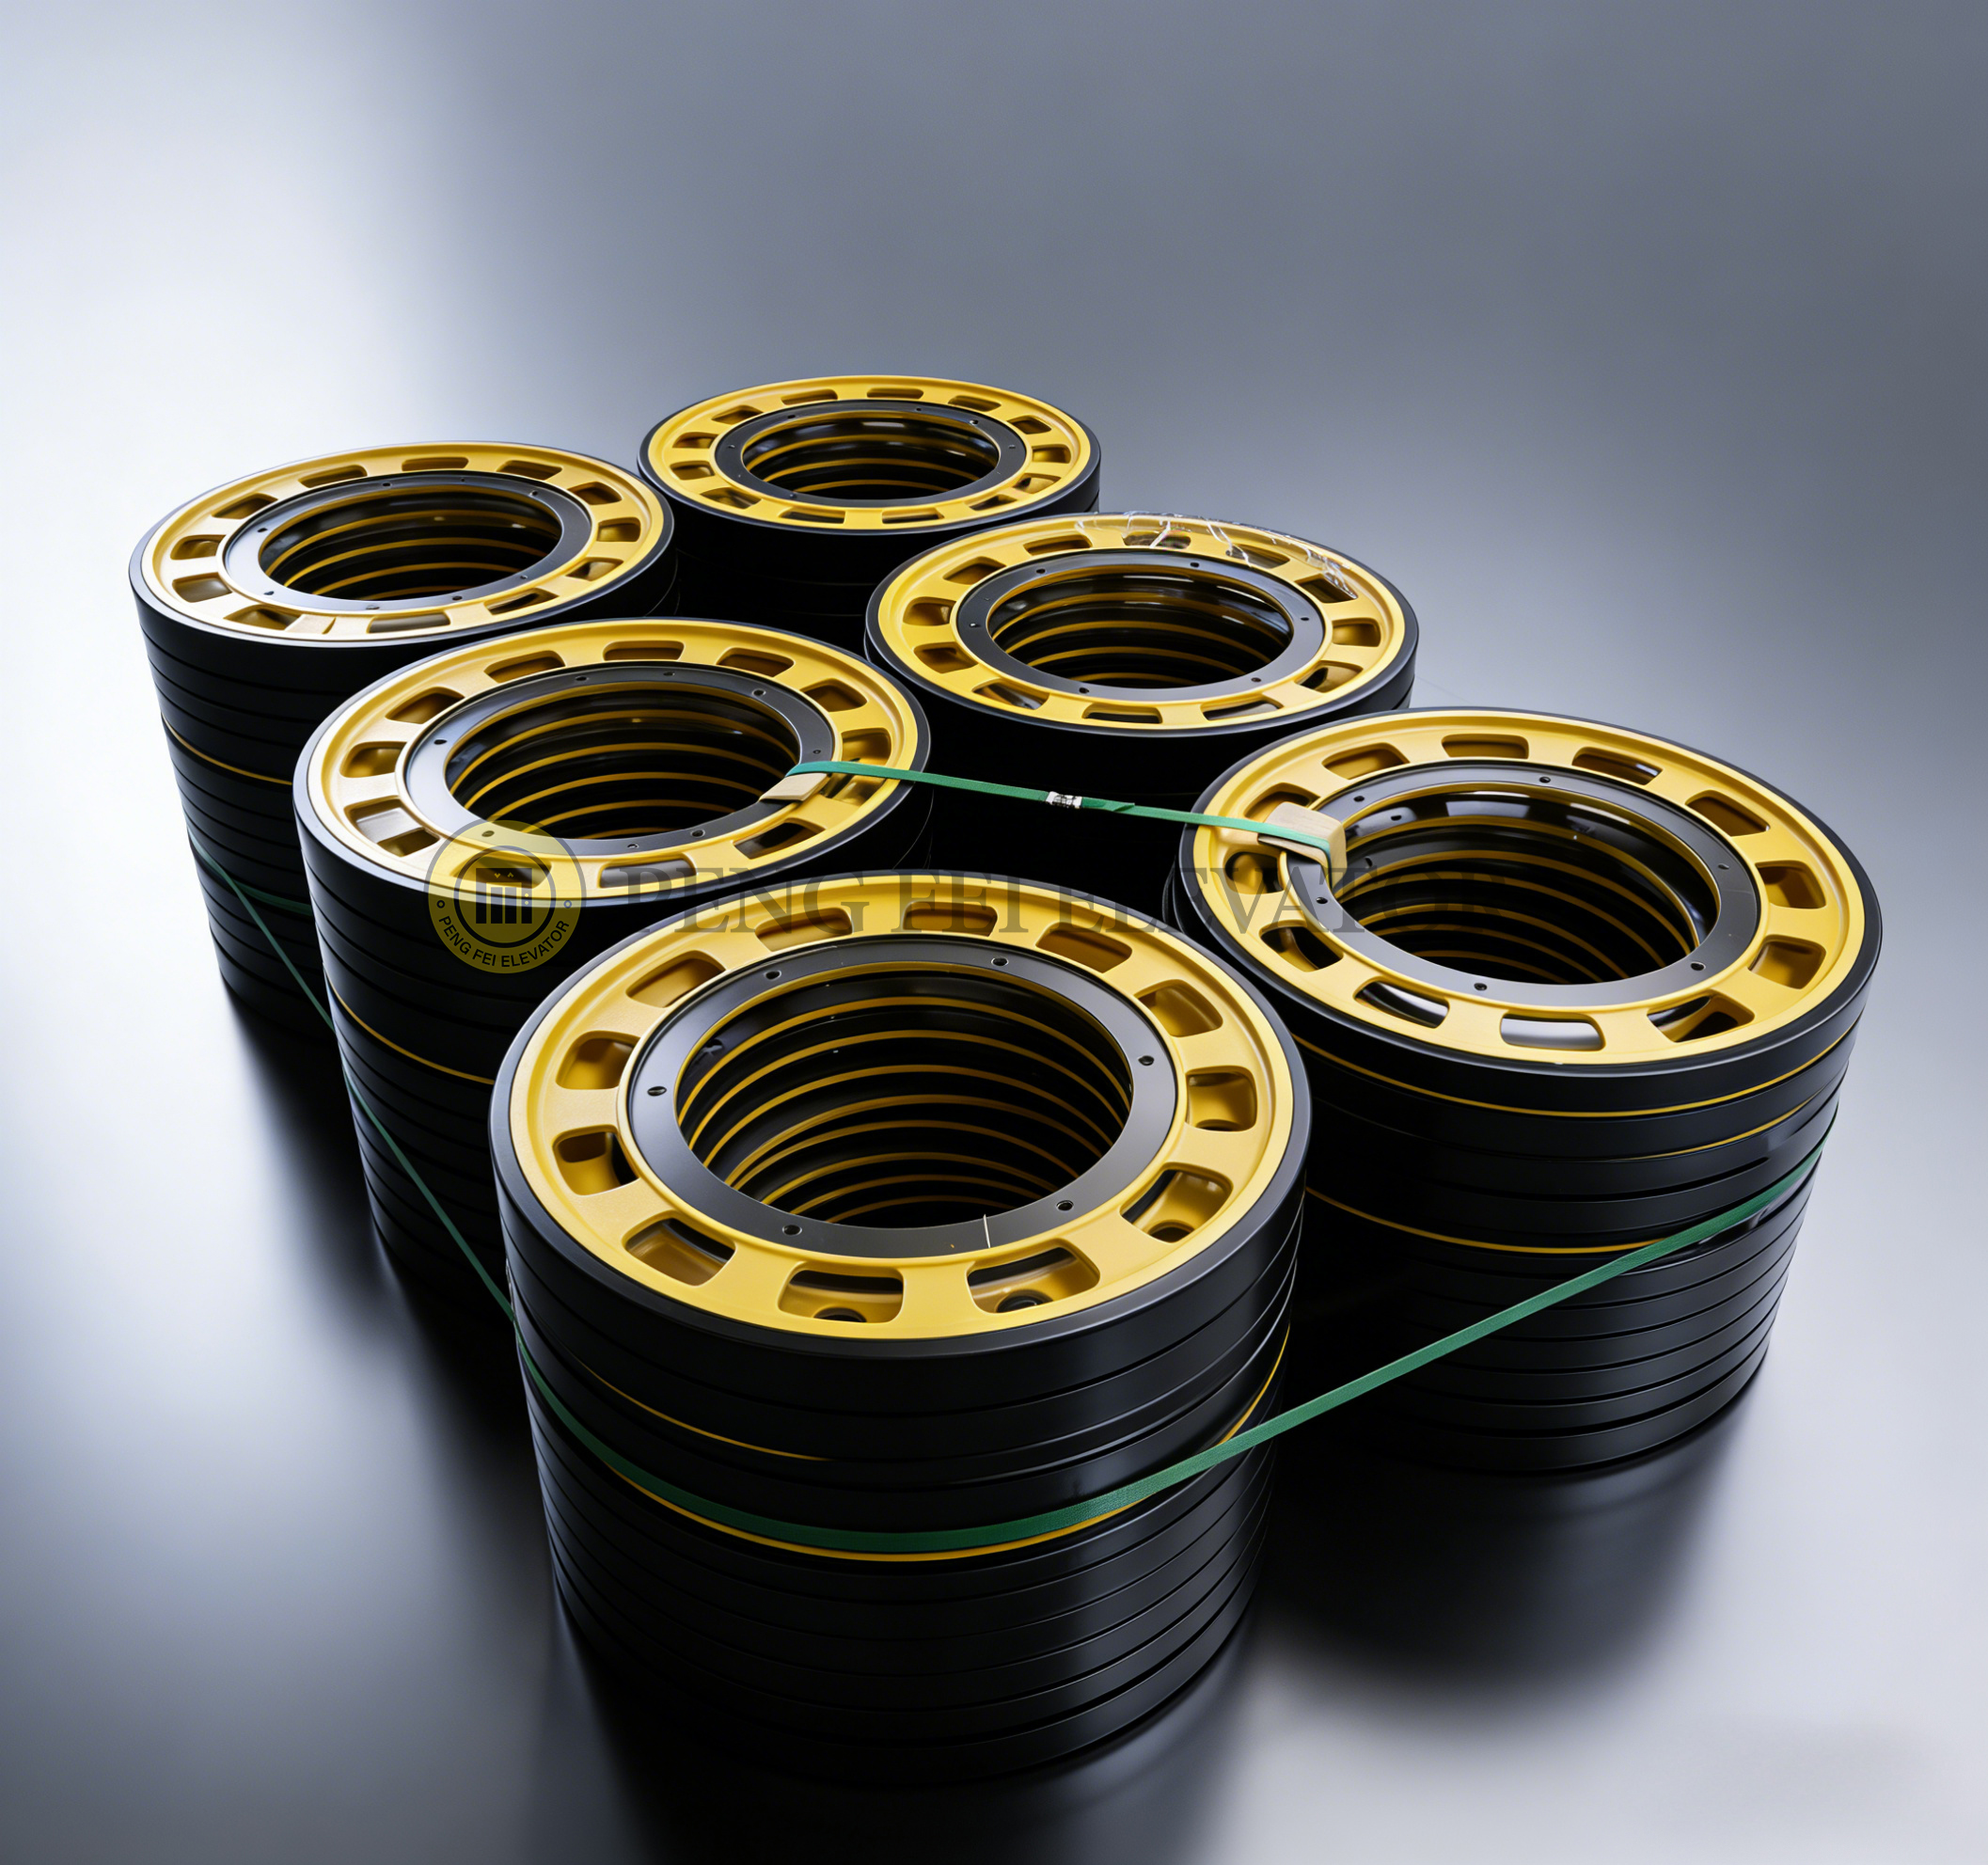
Counterweight blocks are typically stacked within a counterweight frame. The number of blocks used depends on the required balance weight for the specific elevator system. This modular design allows engineers to adjust the total weight during installation or maintenance.
Surface finishing and dimensional accuracy are also important. The blocks must fit securely within the frame to prevent movement during operation. Loose blocks can cause noise, vibration, and potential safety risks.
In addition to standard designs, some elevators use customized counterweight blocks to meet specific requirements. These may include special shapes or materials to fit unique installation environments.
Although simple in appearance, the elevator counterweight block is essential for the safe and efficient operation of modern elevators. Its role in balancing loads and reducing energy consumption makes it a fundamental component in elevator engineering.
We offer various mechanical replacement parts for escalators and elevators. The products include escalator tooth plates, step frame strips, wear-resistant guide rail strips, step rollers, sprockets, driving rollers, driving friction wheels, driving shafts, gear assemblies, step chains, complete chain components, handrail belts, etc. In addition, we also provide elevator wire rope head assemblies, traction machine shock absorbers, car shock absorbers, sliding guide shoes, hollow guide rails, cast iron guide shoe shoes, traction wheels, guide wheels, buffers, etc. All wear-prone components suitable for electric escalators are compatible with mainstream elevator brands and are applicable for equipment maintenance, renovation projects, and new machine assembly. We offer OEM customization services and can handle large-scale orders as well as small-scale repair orders. Our products are of stable quality and the factory direct sales price has a significant advantage.